Severe-Duty Transmissions.
Indian Engineering. A Heritage Since 1970.
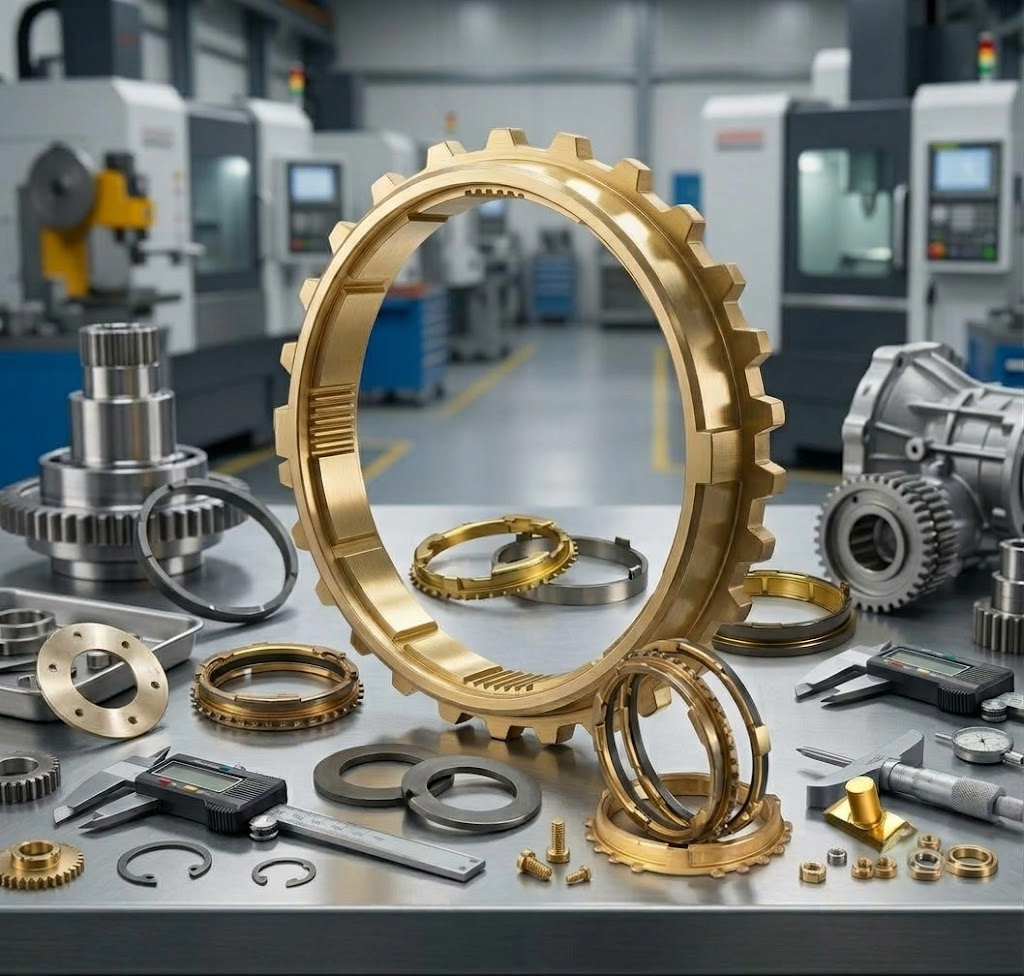
Rishab Export International (REI) engineers heavy-duty synchronizer rings and high-tensile brass forgings for commercial gearboxes, farm tractors, and off-highway drivetrains. By controlling the complete cycle—from raw induction melting to precision CNC turning and broaching—we deliver precise tolerances and zero metallurgical defects.
Thank you for reading this post, don't forget to subscribe!| Primary Alloy Series | CuZn37Mn3 / High-Tensile Manganese Brass |
| Hardness Specification | 170 - 210 HBW / 60 - 68 HRA |
| Cone Angle Precision | Within ± 3 Arc-Minutes (Friction Mating) |
| Global Dispatch | Direct OEM & Tier-1 Transmissions (20+ Nations) |
Pioneered in the 1970s, Engineered for Tier-1 Export
Our family’s manufacturing legacy was established in the 1970s by our grandfather through the inception of the PINKI brand. Built on practical metallurgical knowledge and field-proven reliability, PINKI became an aftermarket benchmark for durable replacement transmission parts.
In 1991, Rishab Export International (REI) was founded to scale this capability into international Tier-1 OEM channels. We centralized operations at our modern Bahadurgarh plant in Haryana—bringing custom alloy formulation, continuous billet casting, closed-die power forging, and multi-axis CNC broaching under full in-house control.
PINKI Brand
The foundational pillar established by our grandfather, providing heavy-duty replacement gears with field-proven endurance.
REI Global Export
Our global export entity engineered for Tier-1 supply, exporting custom-alloy synchronizer rings and precision forgings to 20+ countries.
| Location | Bahadurgarh Industrial Estate, Haryana (Delhi-NCR Corridor) |
| Vertical Continuity | 100% In-House: Virgin Charge → Continuous Billet → Finished Ring |
The 7-Stage Metallurgical Process Flow
Complete control from virgin alloy formulation to oceanic export preservation.
Induction Melting & Spectrographic Verification
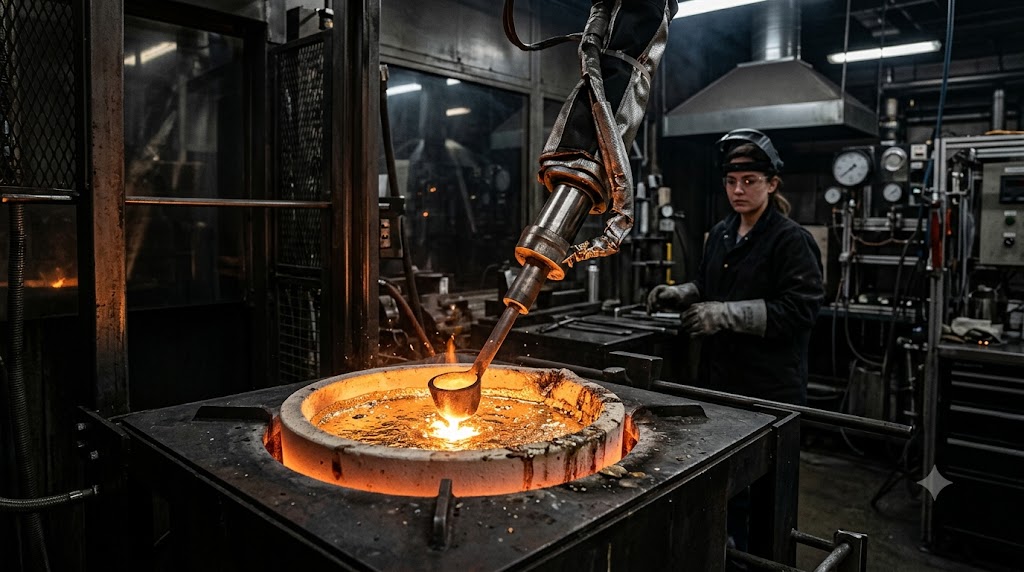
Unlike machine shops relying on generic commercial brass bars, REI alloys raw virgin metals directly in our medium-frequency induction furnaces. We blend electrolytic copper with zinc and micro-alloying elements (Manganese, Silicon, Aluminum) to achieve frictional stability and wear resistance under severe transmission loads.
| Alloy Designation | CuZn37Mn3Al2PbSi (EN 12164 / Special Brass) |
| Testing Protocol | Optical Emission Spectrometer per Heat Charge |
| Target Yield Strength | ≥ 380 N/mm² (Ensures high tooth shear resistance) |
| Quality Guarantee | 100% Batch Chemical Traceability to Raw Ingot |
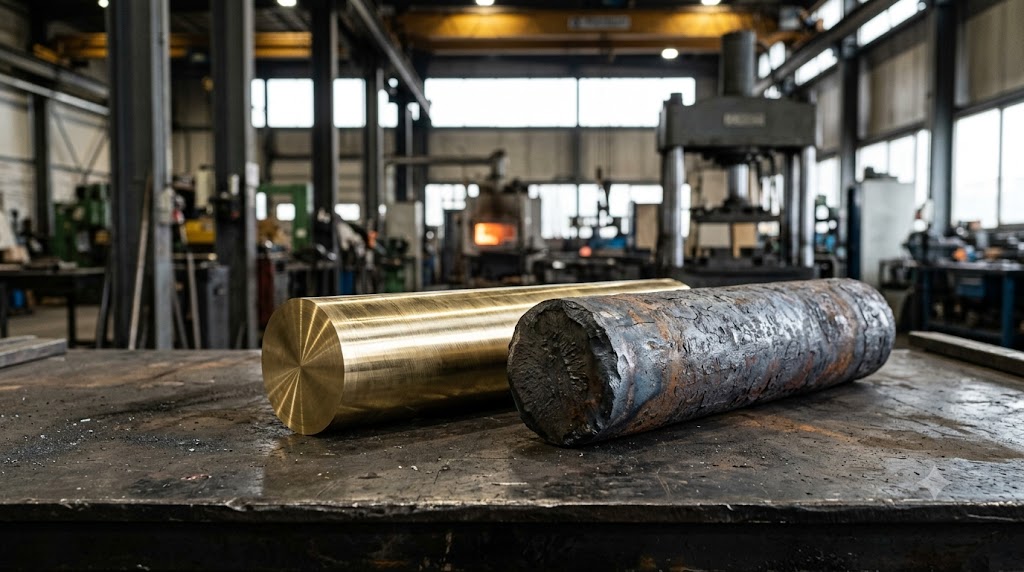
Continuous Vertical Billet Casting & Slug Preparation
Molten brass flows through chilled graphite dies in our vertical continuous casting system. This process ensures a dense, homogeneous crystalline structure free of gas porosity, slag inclusions, or internal voids. Cast billets are then precision-sawn and turned into exact-weight slugs ready for forging.
| Solidification Speed | Continuous Vertical Chilled Extraction |
| Centerline Quality | 100% Solid Core (Ultrasonic Checked) |
| Slug Cut Tolerance | ± 1.5 Grams (Prevents Forging Flash Imbalance) |
| Pre-Forging Finish | Precision Turned to Remove Oxide Skin |
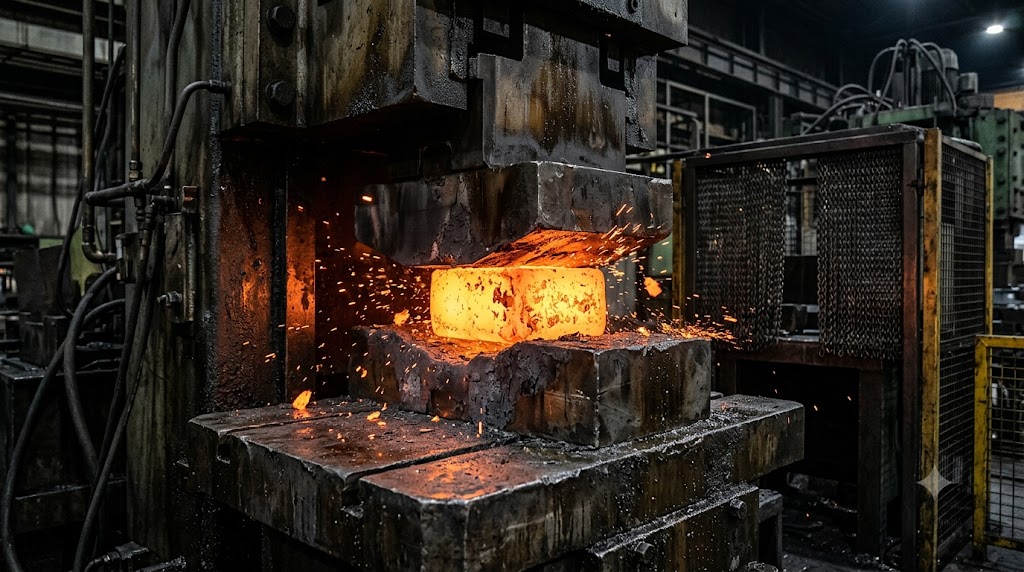
Closed-Die Hot Forging Under High-Tonnage Presses
Pre-cut slugs undergo temperature-controlled induction heating before hot forging under heavy mechanical and friction screw presses (from 200T to 500T). Closed-die compression refines the metallic matrix, yielding unbroken radial grain-flow lines that align with the synchronizer teeth for higher impact resistance.
| Press Configuration | 200T, 315T, and 500T Mechanical & Friction Presses |
| Thermal Monitoring | Closed-Loop Infrared Optical Pyrometry |
| Grain Morphology | Radial Continuous (Zero Grain Cleavage under Shift Shock) |
| Near-Net Forming | High Material Yield with Optimized Flash Channel |
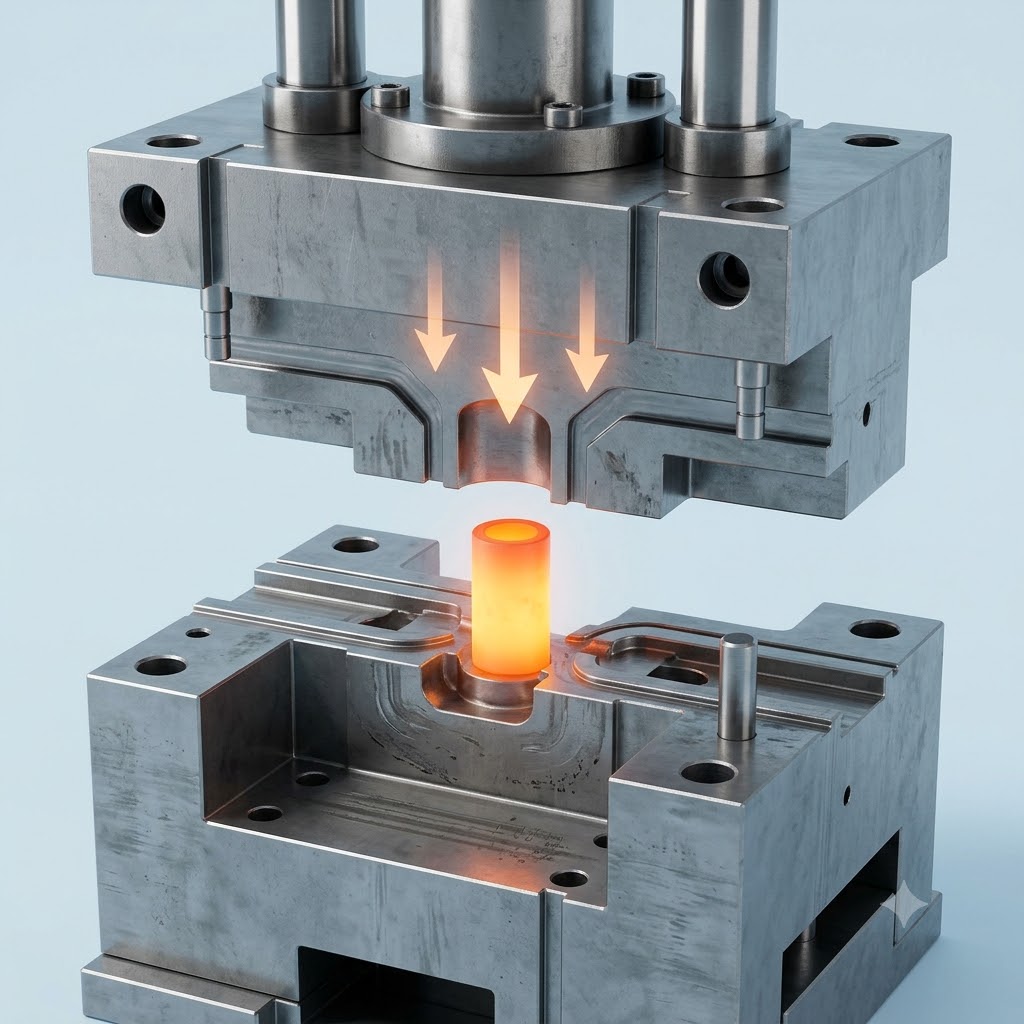
Precision Closed-Die Tooling & Flow Control
We design and machine our closed-die sets in-house using vacuum heat-treated H13 tool steel. Symmetrical die cavities, controlled draft angles, and uniform flash lands guide the heated brass into complex tooth geometries, avoiding cold shuts, flow wrinkles, and stress points.
| Tooling Substrate | Premium AISI H13 Vacuum Quenched & Tempered |
| Die Cavity Hardness | 50 - 52 HRC (Maintains repeatable ring profile) |
| Draft Angle Control | Minimum 1.5° - 2.0° for Clean Ejection |
| CAD/CAM Simulation | Flow-Line Finite Element Analysis prior to Die Cutting |